Get in touch with Wanhui Company

Food packaging permeability describes how gases and/or vapors pass through packaging material. Buyers should compare quantities and environments before ranking reports. A low oxygen value from a dry film test cannot, by itself, establish how a filled tray and lid will perform.
By GW · Updated October 2026
Food packaging permeability is condition-dependent. Match the material, units, method, temperature and humidity before comparing values. Evaluate the closed package and food separately.
Before comparing two reports
- Lower oxygen transmission isn’t the right goal for every food.
- A film result and a whole-package result have different denominators.
- Missing conditions call for clarification; known mismatches may require retesting.
- Barrier performance, seal integrity and food shelf life answer different questions.
| Quantity | Example unit | Read alongside it |
|---|---|---|
| Oxygen transmission rate | cm³/(m²·day) | Film thickness, gas pressure, temperature and relative humidity |
| Water vapor transmission rate | g/(m²·day) | Humidity on both sides, direction and temperature |
| Whole-package oxygen transfer | cm³/(package·day) | Package geometry, closure and the test method’s scope |
| Permeability coefficient | cm³·µm/(m²·day·atm), for example | Homogeneous-material assumption and pressure convention |
Connect Barrier Data to the Actual Food and Storage Route
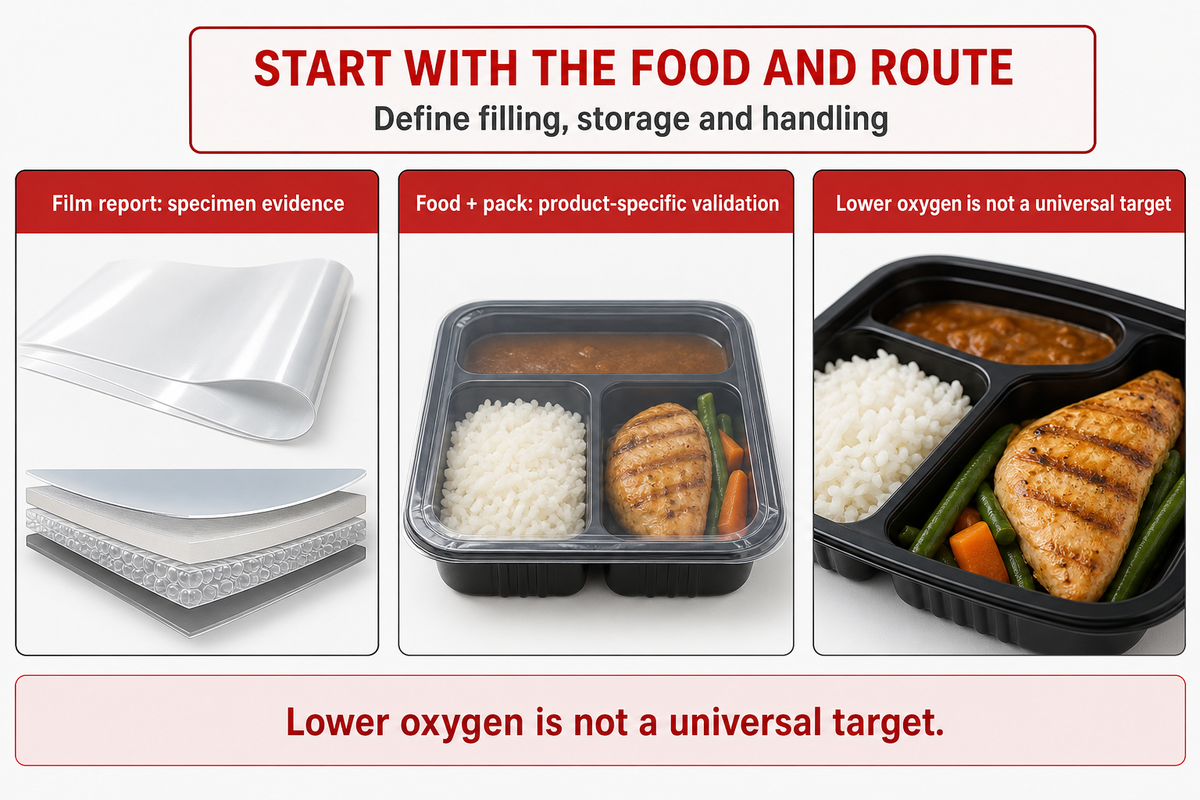
Food packaging performance begins with the food product and its journey to the customer. Determine the food quality change to be controlled and define filling, storage and handling conditions. The result is an application brief which tells the laboratory the comparison to be made, and procurement which claims require supporting evidence.
A dried snack can gain moisture and lose its crispness. A prepared meal can lose moisture and exchange it with other ingredients. Condensation is possible inside a package. Consider how much oxygen entered through the package, and how much was present at the time of filling. Those are different contributions to the same product shelf life decision.
A container that’s designed not to let liquid drip out doesn’t thereby establish its water vapor permeability or gas barrier properties. Treat the container family as the starting point. The broader disposable food containers guide covers format selection; barrier reports address a narrower part of that choice.
Food science changes the oxygen target
Respiring produce makes a universal lowest-oxygen rule unreliable. In Dai and colleagues’ 2023 fresh-cut broccoli experiment, each PET pack contained 200 g of broccoli and was stored at 4 ± 0.5 °C. Directly sealed controls developed lower oxygen and higher carbon dioxide than the study’s oxygen-filled treatment, and had poorer sensory results. This study shows evidence of changing atmospheric conditions. It doesn’t establish the optimal gas mixture for other foods. The study didn’t test films of different oxygen transmission rates.
For raw fish, a different kind of limit is relevant. The US Food and Drug Administration’s Import Alert 16-125 examines the risk of botulinum toxin in fish in reduced-oxygen environments. A buyer should not turn that fish-specific guidance into a general oxygen limit for prepared meals. A food safety assessment is specific to the product and process. The food and packaging must be evaluated together when establishing the usable life of food products.
A hypothetical customer transports a 450 g chilled meal over a short local delivery route, and is now moving it over a long distribution route. Purchase receives a lower quote for trays with the same nominal footprint. Production is holding on to its closure operation, and Quality Assurance needs justification for a changed route. Ordering the tray immediately would leave the decision resting on its appearance. A good initial request would identify the meal and provide the actual time-temperature history and filling mass, the construction of the lid and the route it took through the facility. The supplier can then distinguish an existing report that answers the question from a test that still needs commissioning. In this example, no storage duration or temperature is a validated food-release condition.
For the 450 g meal, a report for an empty film specimen leaves the food load, headspace and closure unanswered. Address those application gaps before giving preference to a lower transmission value. The good purchase is an evidence package that’s comparable to the intended route, followed by product-specific validation.
Read the Units Before Comparing Barrier Numbers
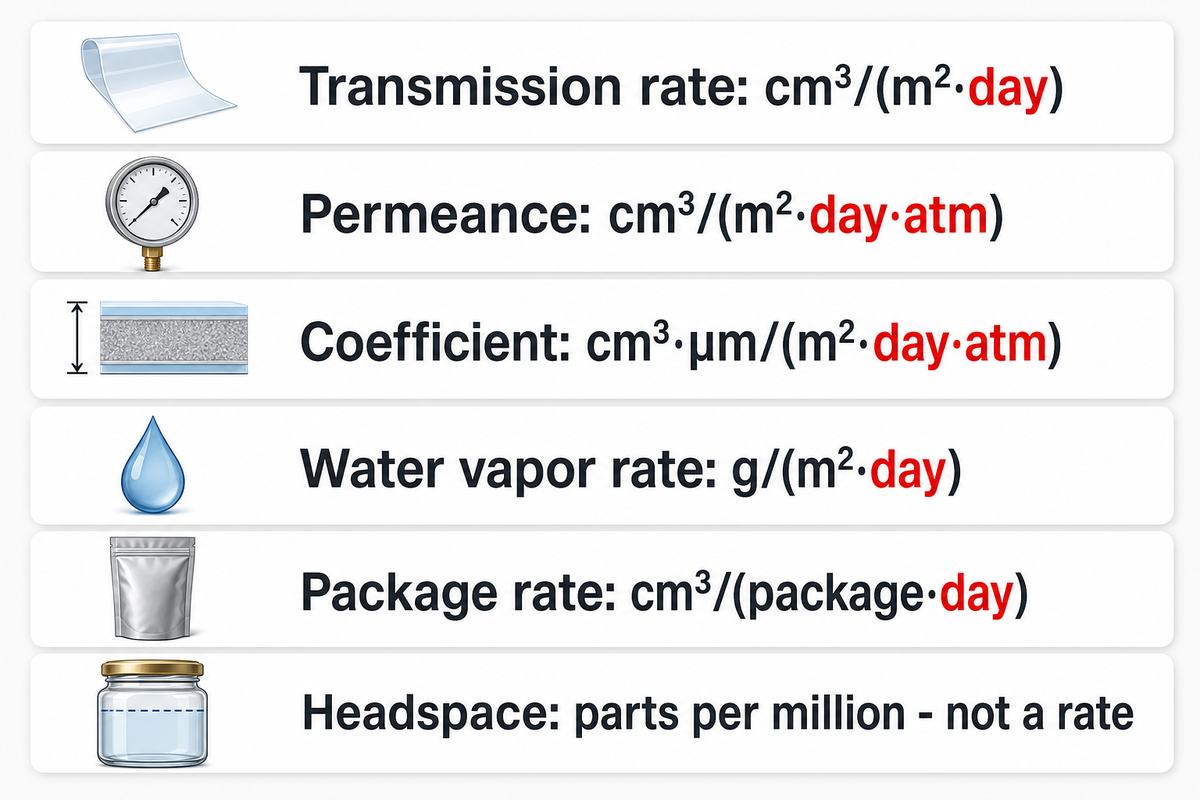
Transmission rate, permeance and permeability coefficient describe related quantities with different normalizations. Transmission rate describes passage through the tested specimen under specified conditions. Its quantification needs a stated area, time and unit. Permeance accounts for the driving pressure difference; a material permeability coefficient also accounts for thickness under appropriate assumptions. Keeping these distinctions helps prevent false supplier rankings.
Differing partial pressures of gas across a barrier cause movement. Small molecules interact with polymer and are thus able to pass through it. Permeant means “species being measured,” for example, “oxygen.” A film can be permeable to several species at different rates. A result for one gas can’t be extrapolated to another. Thus, evidence for carbon dioxide and evidence for oxygen will be examined separately to account for their effects on packaging application.
| Report wording | What it can tell you | What must still match |
|---|---|---|
| Transmission rate, cm³/(m²·day) | Gas volume per tested area and time | Gas, thickness, pressure conditions and environment |
| Permeance, cm³/(m²·day·atm) | Gas transfer normalized to a pressure difference | Material construction, temperature and humidity |
| Coefficient, cm³·µm/(m²·day·atm) | Thickness-normalized behavior within the model used | Homogeneity and the model’s validity |
| Water vapor rate, g/(m²·day) | Mass transfer per tested area and time | Water-vapor gradient and temperature |
| Package rate, cm³/(package·day) | Transfer attributed to the tested package | Geometry, closure and conditioning |
| Headspace concentration, parts per million | Composition at a measurement time | Headspace volume and time history; it is not a rate |
The discussion by the Institute of Food Technologists for multilayer transmission calculations illustrates how terminology and equations often confuse readers. Copy the quantity name and complete unit from the report. A column in a spreadsheet labeled only “permeability” reveals nothing about whether pressure or thickness has been reported. Keep the original permeability data with the comparison.
Units show that comparisons between packaging films and complete packages are misleading. An area-normalized value for a film can’t be compared with a package-normalized value without a model that justifies the comparison. Corners, walls, lids, and seals contribute differently. Multiplying a film value with the nominal surface area of a tray is an estimate and an assumption, not a measure of a pack.
How is permeability calculated?
A permeability coefficient for a homogeneous film can be calculated as P = J × L / Δp under steady-state conditions, where J is the measured transmission rate per unit area, L is film thickness and Δp is the permeant’s partial-pressure difference. The units must be consistent, and the assumptions must match the nature of the material and the measurement.
For a deliberately hypothetical film, let J = 2 cm³/(m²·day), L = 50 µm and Δp = 1 atm. Then P = 2 × 50 ÷ 1 = 100 cm³·µm/(m²·day·atm). At a thickness of 25 µm, that same idealized coefficient predicts J = 100 × 1 ÷ 25 = 4 cm³/(m²·day). Doubling the predicted rate follows the assumed model; it isn’t measured proof that thinning a commercial laminate produces that result.
A multilayer structure, a humidity-sensitive coating, or a damaged film, for example, may not be compatible with this straightforward estimation. It’s appropriate to ask the laboratory which coefficient it reported and the assumptions it made before using the number in a purchasing specification.
There are several ways of expressing pressures that may warrant further evaluation. For example, a supplier may state an oxygen transmission rate under a specified test atmosphere, while another supplier may express the value as a pressure-normalized quantity. Dividing a number by pressure again would apply the correction twice. Keep the uncorrected value and any converted value with the equation and assumptions.
A hypothetical 50 µm film producing 2 cm³/(m²·day) at a 1 atm partial-pressure difference gives a coefficient of 100 cm³·µm/(m²·day·atm). The calculation helps audit units. It doesn’t predict oxygen exposure inside food without the package geometry, initial atmosphere and other relevant pathways.
Oxygen Transmission Rate Tests: ASTM D3985 and Humid Conditions
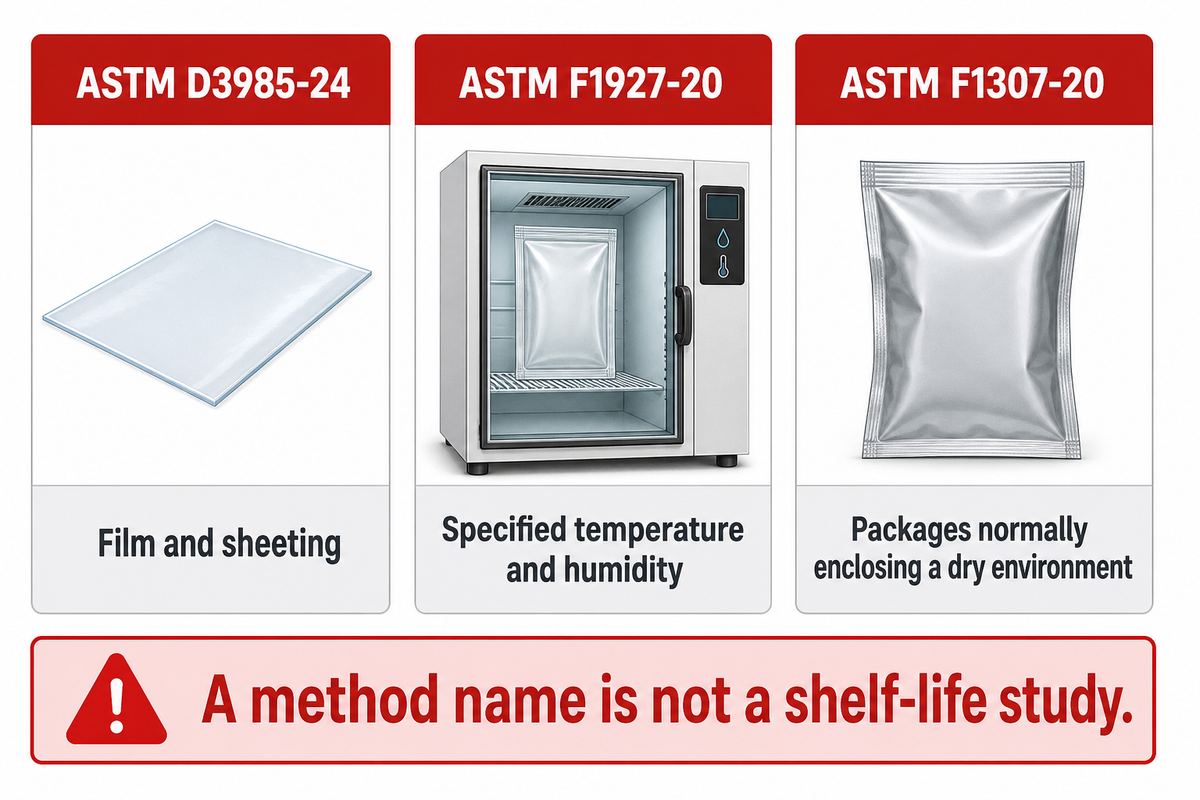
An oxygen permeability test is useful only within its scope. Check the edition and compare the methods, temperature, relative humidity, and gas composition and pressure. The laboratory should be able to provide an explanation regarding the reason for using those conditions, and where the result is valid.
| Method | Public scope in brief | Buyer boundary |
|---|---|---|
| ASTM D3985-24 | Oxygen transmission through film and sheeting, including specified multilayer and coated materials | Do not label a complete tray-and-lid system tested because its film was tested |
| ASTM F1927-20 | Steady-state oxygen transmission at specified temperature and relative humidity | Record the humidity conditions rather than assuming dry testing |
| ASTM F1307-20 | Oxygen transmission through packages normally enclosing a dry environment | Discuss suitability with the lab before applying this scope to a humid meal |
The public pages for ASTM D3985-24, ASTM F1927-20, and ASTM F1307-20 provide information about the boundaries. A method number is evidence about the measurement procedure. It does not confirm that a supplier is “ASTM-certified,” and it does not transform a film test into a shelf-life study.
“The OTR is an important determinant of the packaging protection afforded by barrier materials.”
Discussion from ASTM indicates that OTR is not the only determinant of the protection afforded by a barrier film. Reliance should not be placed on an OTR quotation which includes a low number but does not describe the sample. Request the report’s specimen record before applying the number to the purchase.
Suppose one laboratory reports a film at 23 °C and 0% relative humidity while another tests at 23 °C and 50% relative humidity. Equal temperatures do not make the two reports equivalent. Water absorbed by a humidity-sensitive layer can alter its transport behavior. Ask for matched conditions or an explanation supported by the material’s own data; don’t invent a correction factor.
A buyer may say that the additional cost and time for a new test is unnecessary. Resolve the cheapest uncertainty first: A humidity field missing from the sample may be evident in the laboratory record. A confirmed condition mismatch is different. It should be decided by quality assurance if evidence is sufficient to resolve the uncertainty or if a matched test is needed.
Comparing 23 °C/0% relative-humidity data with 23 °C/50% data leaves a material question unresolved even when both reports use the same gas. Identify missing conditions before scheduling the next test. Retest when the difference matters to the decision and a supported comparison can’t be established.
Moisture Barrier Packaging: Read Water Vapor Conditions
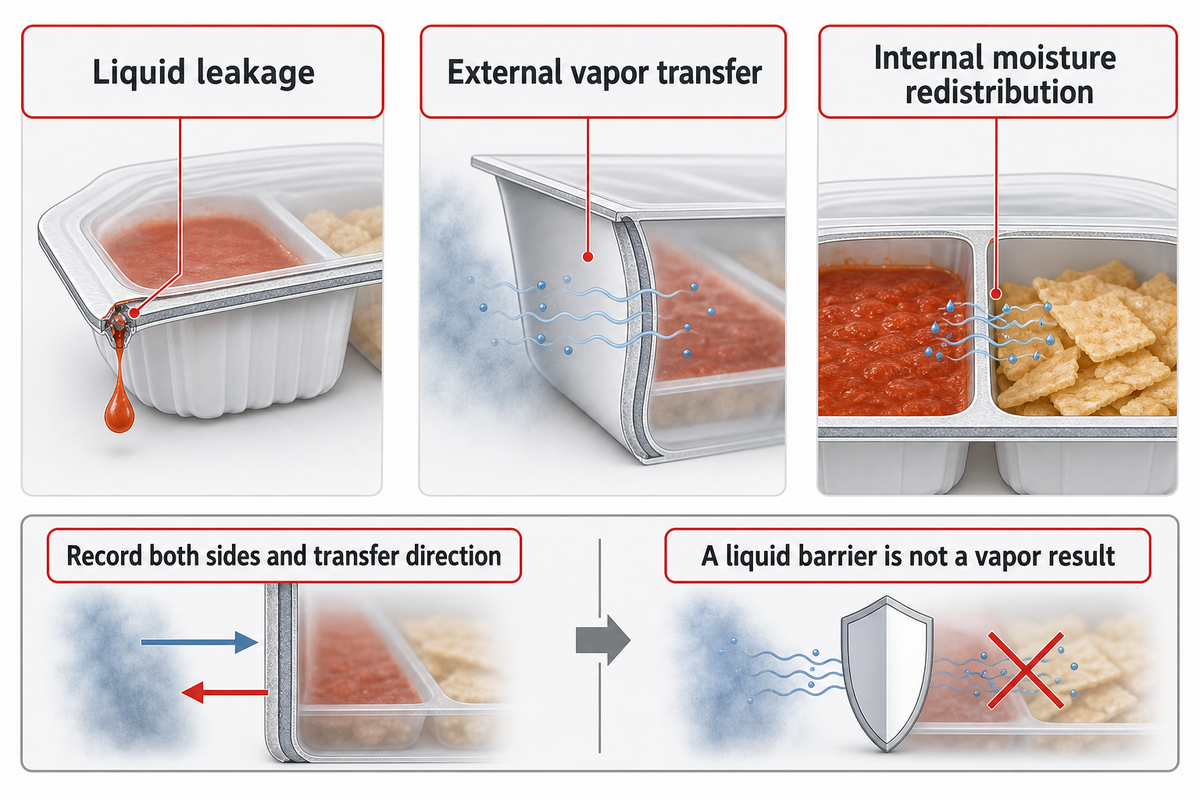
Barriers to moisture work on the basis of the driving force of water vapor and how material is exposed to it. Record conditions on both sides of the barrier and the direction of the transfer. Just because a package keeps a liquid from penetrating it doesn’t mean that package prevents vapor transmission. An outer barrier can’t prevent moisture from transferring between food items.
The current ASTM F1249-25 public scope covers water vapor transmission rate through flexible barrier materials up to 3 mm thick. The caution provided on thickness and the relationship of water-vapor partial pressures is useful for interpretation of reports; proportional scaling does not always apply. It is better to request the tested thickness. Improvement in performance of a moisture barrier is not necessarily proportional to an increase in thickness of the barrier.
Water vapor barrier properties require an exposure description. “High water resistance” can refer to liquid contact, while a high water-vapor gradient describes the measurement’s driving force. Neither phrase tells a buyer the measured mass transfer. The response of packaging materials to water must be stated in terms that match the problem being investigated.
A report measured across 90% and 0% relative humidity at 38 °C isn’t interchangeable with one measured across 50% and 0% at 23 °C. The temperature changes the vapor-pressure difference as well as the material response. Converting the printed humidity percentages into a ratio and scaling the rate would conceal those effects. Send both complete reports to the testing laboratory if a comparison is commercially important.
In Packaging World’s vapor transmission discussion, Sterling Anthony highlights reporting conventions including g/m²/day and g/100 in²/day. An area conversion is a unit conversion; it doesn’t correct differing environmental conditions. Keep those two operations separate in the comparison worksheet.
Where a good moisture barrier still leaves a problem
Claire Koelsch Sand’s IFT article on controlling moisture describes moisture movement and the misleading apparent barrier performance of some edible films under restricted water-activity gradients. A coating with a tendency to adsorb water can behave differently, depending on exposure. Ask whether the material under consideration is bio-based and if the result is relevant over the range of interest.
We also need to account for the movement of moisture within a package. A crisp component stored next to a wet component can affect the texture of the crisp component even if little moisture crosses the package. Increasing the outer barrier won’t answer a compartment design question using the information available in the cases presented. The arrangement of the products, moisture content and the food’s water activity need to be reviewed in the application.
If a supplier claims that a thicker lid solves the problem, define which failure it addresses. A test method’s scope has a 3 mm thickness limit; a recommended lid thickness isn’t the same thing. Separate liquid leakage, external vapor transfer and internal moisture re-distribution, then choose the evidence that best supports the suspected pathway.
Compare PE, PP, PET and Coated Fiber by Construction
Permeability of various material families provides a basis for classification of options. However, a universal reliable basis for comparison is lacking. Other factors like grade, thickness, and added layers may affect the result. Consider the proposed construction and measured conditions, then check whether forming or closure operations altered the specimen being represented by the supplier’s report.
Polymer properties explain why one label is incomplete. Higher crystallinity may obstruct some transport pathways, but a grade description alone doesn’t define the final film. An additive may alter the polymer, and thermal and/or moisture history may also alter the final film. Tensile strength, elongation and heat resistance also answer different questions from oxygen transfer. Purchasing needs the thermal and mechanical evidence relevant to use, along with the barrier result, to prove the product is suitable for its intended purpose.
| Material or structure | Information to identify | Useful comparison | Limitations / Not suitable for |
|---|---|---|---|
| LDPE film | Low-density polyethylene grade and thickness | Same-condition oxygen and vapor results | A generic low density polyethylene label is not a measured value |
| HDPE film or sheet | Grade, orientation and formed-wall distribution | Evidence for the proposed specimen | Resin-level data cannot establish a finished container result |
| PP film | Cast or oriented polypropylene, grade and thickness | Like-for-like film data | PP is too broad a label for an unconditional ranking |
| PET film or sheet | Grade, coating and orientation | Specified construction before and after relevant processing | A flat sheet does not represent every formed corner |
| Polystyrene structure | Grade, solid or foamed form, geometry | The supplied structure rather than the resin name | Appearance does not establish oxygen permeability |
| Polycarbonate article | Exact grade and intended application | Product-specific evidence and use limits | Thermoplastic family alone gives no food-contact permission |
| Ethylene vinyl acetate layer | Copolymer grade, role and thickness | The complete laminate in which it is used | A seal-layer name does not describe every barrier layer |
| EVOH multilayer | Ethylene vinyl alcohol grade, barrier thickness and surrounding layers | Humidity-conditioned complete structure | Dry gas data alone may miss the intended moisture exposure |
| PVDC-containing laminate | Polyvinylidene chloride layer and total structure | Matched film and processing conditions | An acronym does not establish end-of-life suitability |
| Coated fiber or PLA-lined fiber | Substrate, coating coverage and liner identity | Exact supplied construction and closure | Liquid resistance is not a vapor-transmission result |
| Metal-oxide-coated film | Coating, substrate and post-process state | Evidence that accounts for coating defects | Nominal layer composition may hide microscopic damage |
Which is better, PE or PP plastic?
PE and PP can’t be ranked for food packaging from their names alone. A useful choice compares actual grades and constructions at matched thickness, temperature and humidity, then considers forming, closure and intended use. Select the structure that meets the product’s defined requirements with supporting evidence, as opposed to the polymer with the most favorable generic chart.
A thinner-oriented PP film, a thicker PP tray, and a low-density polyethylene seal layer are three different structures with different functions. A supplier should identify which of the three its report covers. If the proposed package changes both resin and thickness, request data for the new construction instead of attributing the change to resin. High gas permeability may be undesirable for one application and part of the gas exchange for another. A label such as high permeability still requires a gas and a measured condition.
A published material map is useful for screening, with limits. Yeh and Turan’s 2026 gas-permeability mapping study combined literature data and used assumptions where thickness or test conditions were missing. Its material clusters are a research comparison, not verified performance for a purchasing specification. Read the provenance of a chart before treating apparent precision as measured equivalence.
The Wonhi bagasse and PLA-lined clamshell catalog illustrates the identity problem. It lists WH-BG-88-1C and WH-PLA-88-1C in an 8 × 8 × 3 in format, with bagasse and bagasse-plus-PLA-liner constructions respectively. Those catalog descriptions identify two different products. They don’t supply matched oxygen or moisture measurements. The public Wonhi pages reviewed for this guide don’t establish a tested high-barrier tray-and-lid combination; request the matching product and laboratory records before making that selection.
An 8 × 8 × 3 in format can therefore describe more than one construction. If a buyer wants to replace a tray without changing the case layout, retain the dimensional requirement while requesting the new SKU’s barrier and closure evidence. Equal footprint doesn’t establish equal protection.
High Barrier Film: Check the Layer Stack and Moisture Response
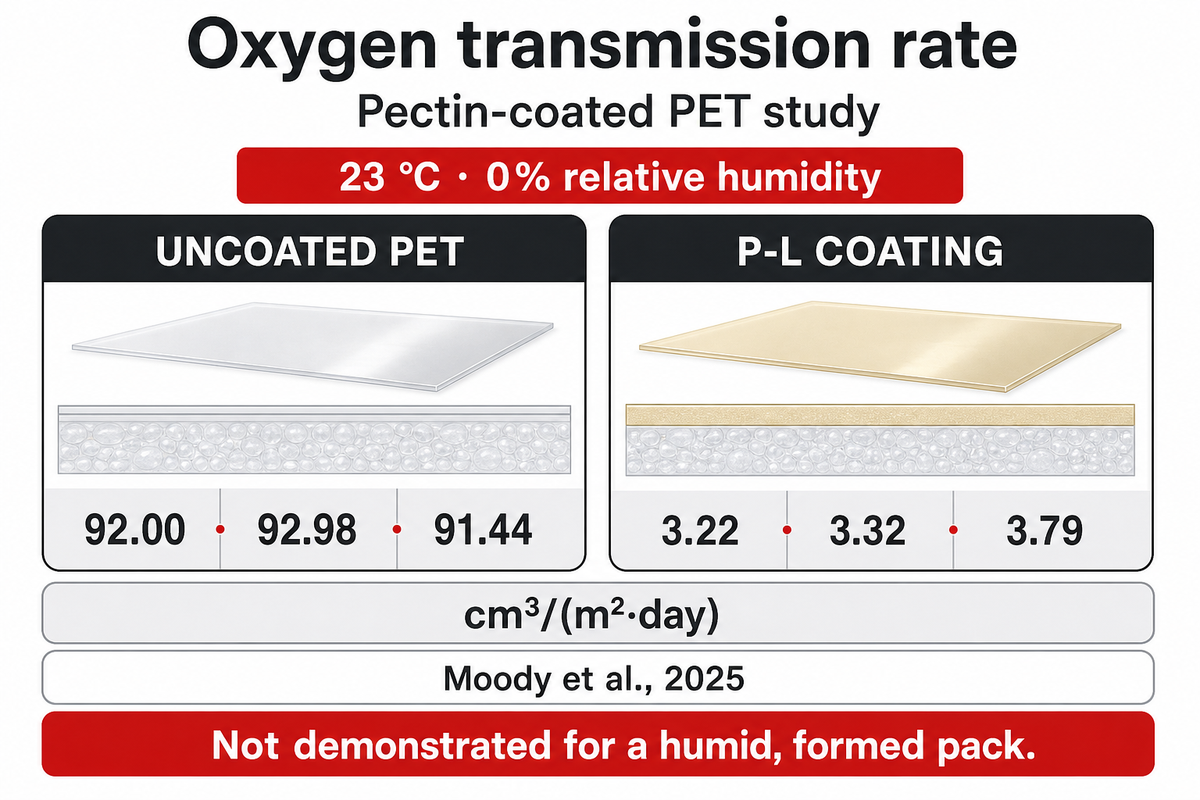
In a multilayer high barrier film, the layers serve different functions. Identify the gas-barrier layer, the supporting substrate, and what faces the food and the environment. Determine how moisture gets to the sensitive layers and if the measured sample was exposed to the forming, heating and flexing of the packaging.
Multilayer packaging is often a structure layer, adhesive, tie layer, gas barrier and a sealant. A laminate drawing makes those roles visible, but it cannot replace a transmission result. “High gas barrier” describes a function claim; the film report needs to state the gas, conditions, and construction that was tested.
EVOH is ethylene vinyl alcohol. The moisture response is one of the reasons to analyze the entire layer stack and condition the layers rather than relying on a dry film. The surrounding layers affect exposure and the thickness of layers is important. Separate questions on oxygen and water vapor, even if they’re in the same supplier data sheet.
A laboratory example demonstrates the limit and the potential of a coating. Moody and colleagues’ 2025 pectin-coated PET study reported uncoated PET readings of 92.00, 92.98 and 91.44 cm³/(m²·day), compared with 3.22, 3.32 and 3.79 for its P-L coating. Measurements were made at 23 °C and 0% relative humidity. Humid formed-pack performance remained outside the demonstrated result.
The same paper reports two P-IPA readings as less than 0.05 cm³/(m²·day), with a third at 0.22. An exact average can’t be computed with those censored readings. When reporting a value that’s less than a detection limit, don’t alter or remove the less-than sign. Preserve the less-than signs and the detection limit when transcribing a report; replacing them with zero or 0.05 silently changes the evidence.
Common failure modes after conversion
Coating continuity can matter as much as its nominal chemical identity. Ashutos Parhi’s 2021 Washington State University dissertation abstract reports that microscopic cracks and pinholes in metal-oxide-coated films can increase oxygen and moisture permeability. That abstract supports a defect-related caution; it doesn’t give a universal damage tolerance for commercial packs.
When considering a particular structure, it’s important to understand what state of processing the supplier was testing. Flat film before conversion may answer different questions compared to film after a heat cycle or material removed from a formed part. Defects in films may be present for a number of reasons. This is a reason to evaluate post-process testing to demonstrate compliance. Not all coatings will necessarily fail.
A frequent purchasing blunder is to pay for another nominal barrier layer without investigating the reason for failure of the previous barrier layer. Quality assurance can first distinguish a material-transmission question from a seal-channel question, while production captures the processing and handling sequencing. If the supplied evidence covers only unprocessed film, a claim about the complete pack needs further evidence. Change in coating, forming or closure should be considered as a defined change in the test question.
Results at 23 °C and 0% relative humidity can justify further investigation of a coating under those conditions. The results can’t define the value of the coating in a humid, formed tray. Ask for evidence on the proposed layer stack after relevant processing before paying for a high-barrier upgrade.
Verify Tray, Lid and Supplier Evidence Together
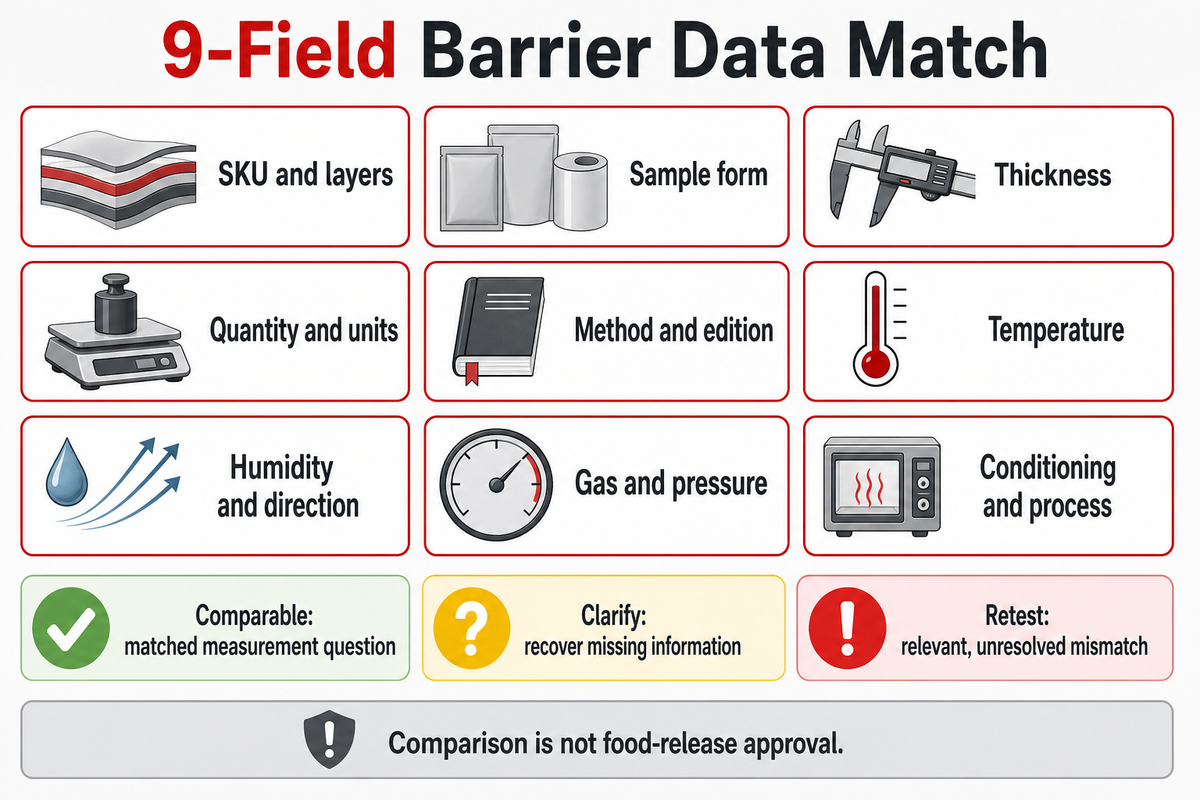
The supplier evidence should identify the exact specimen before interpreting the oxygen/moisture results. Evaluate the tray, lid and closure as a system and distinguish material transmission from leakage. Complete evidence reduces uncertainty in a measurement, but doesn’t make every downstream purchasing or food release decision automatic.
9-Field Barrier Data Match
The 9-Field Barrier Data Match routes supplier reports to Comparable / clarify / retest by checking specimen identity, measurement and exposure conditions.
Use the following filled comparison as a reading exercise. Reports A and B are made-up; their values don’t come from Wonhi test results. The objective is to identify equivalent or comparable data that can be analyzed prior to spending test or material selection budget.
| Field | Illustrative report A | Illustrative report B | Limitations / next decision |
|---|---|---|---|
| SKU and layers | Film A: PET/adhesive/PE | “Barrier lid,” layers omitted | Clarify identity; a trade description is insufficient |
| Sample form | Flat lidding film | Formed tray | Retest the intended comparison; these are different specimens |
| Thickness | 50 µm total; individual layers listed | 50 µm nominal; no layer split | Clarify measured thickness and layer allocation |
| Quantity and units | 2 cm³/(m²·day), oxygen | 2 cm³/(package·day), oxygen | Do not rank the equal numbers; the denominators differ |
| Method and edition | ASTM D3985-24 | “ASTM oxygen test” | Clarify the full method and edition |
| Temperature | 23 °C | 38 °C | Seek matched-condition data; no improvised temperature correction |
| Humidity and direction | 0% RH on both sides; faces labeled | 50% RH; side not identified | Clarify both sides, then assess whether retesting is needed |
| Gas and pressure | Oxygen; Δp = 1 atm stated | Gas and pressure omitted | Clarify composition and pressure convention |
| Conditioning and process | Unformed, unheated specimen | After forming; history incomplete | Define the relevant post-process state before comparison |
“Comparable” means the reports answer the same stated measurement question with sufficiently matched conditions. It doesn’t mean that either value meets the requirements of the food application. “Clarify” means that a field may be recoverable from the existing record. “Retest” means that a difference is known and can’t be resolved with a supported comparison and is pertinent to the decision. The laboratory and quality lead should make this determination.
Keep measured replicates and the reporting limit with the headline figure. A single mean can mask both variation and censored results. Also ask if a nominal thickness was drawn or measured. Those questions are typically more productive than requesting yet another decimal place.
Four evidence tasks with different owners
Evaluation of material transfer through a defined specimen is a material testing responsibility. Closure evaluation covers opening and unintended paths. Shelf-life work evaluates a packaged product over its defined use and distribution. Food-contact review covers use and substances. Purchasing can coordinate the records, but each task needs its own acceptance basis. In the food industry, a materials test and a food-release decision have different responsibilities.
According to the FDA’s guidance on food-contact material components, authorization is tied to the substance, specifications, and intended use. Certain food-contact notifications are also manufacturer specific. Ask for evidence that applies to the supplied construction and intended contact with food. A general company statement does not respond to that request.
There are differences in closure between a snap-fit lid and a heat-sealed lid. The properties of the pack closure and how seal regions are kept clear need to be described, along with the orientations the pack will experience in shipping and handling. Peel resistance, in and of itself, doesn’t eliminate a channel leak. “Leak proof” shouldn’t be accepted as a specification. The scope and acceptance criteria of the test should be evaluated.
Suppose a purchasing team receives two film reports showing the same 2 cm³/(m²·day) result. One covers an unformed sample at 23 °C and 0% RH; the other describes a different laminate but omits humidity. Finance sees no reason to request additional testing because the headline numbers are the same. Quality Assurance asks the second laboratory for the missing conditions and specimen details. If the missing information resolves the question, the team has avoided a duplication of the test. If the missing information describes a different construction and/or environmental conditions, the purchasing team may request a comparison test. The next test would reflect the closure and forming sequences used in the production of the pack being evaluated.
The nine-field exercise is complete when each difference has a decision and an owner. It’s important that unfavorable findings and differences be retained. Those values may explain the reason a sample was accepted for further evaluation or why a sample is being held.
Two reports that show 2 cm³/(m²·day) are comparable only after checking specimens and conditions. Lack of information may mandate an email. An explicit mismatch may justify a test. Neither decision replaces a separate evaluation of the assembled package, food contact or intended shelf life.
Packaging Technology Changes: Recheck Evidence After a Redesign
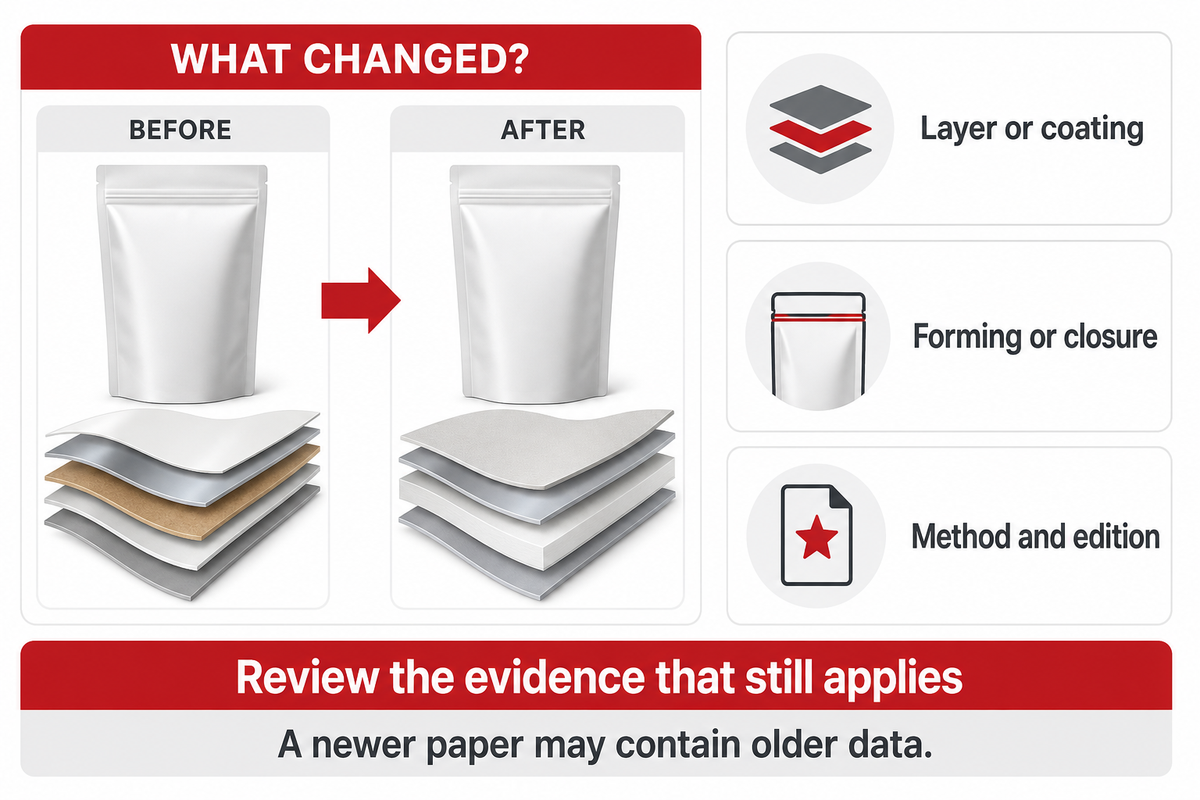
Regarding the food packaging industry, a change in construction should mandate a review of evidence that still applies. Thinner walls and a different coating may affect the specimen represented by a report. Provide both the old and new constructions, so the supplier can identify the variable that changed and justify evidence that still applies.
Recent studies should be read in the context of the underlying data. The 2026 gas mapping study, for example, compiled published data instead of testing a new commercial tray range. The dataset began with 49 studies. The authors identified 295 permeability data points, from which they retained 249 to cluster, making assumptions for the missing data. Just because a study is recent, it doesn’t mean the data is recent and comparable.
The 2025 pectin study also provides another kind of evidence. Its coating results may prompt a development question. However, they may not be transposed to a molded fiber because both contain plant derived material. The substrate, coating coverage and intended environment must match the claim.
In cases where a standard is revised, this also belongs in change control. The official F1249 webpage lists the 2025 edition while older trade discussions may list the previous edition. Report the edition and ask the testing laboratory about comparability. This listed ASTM F1249 edition was used for the comparisons in this document. An edition date alone is not evidence that a material’s performance improved or that every earlier report is invalid.
In cases where there are changes in the manufacturing of food contact materials, define the layer, forming, or closure that’s being changed. If procurement is proposing a change to a 50 µm layer to a 40 µm layer, define the layer to be changed before applying a materials model. The commercial benefit is a valid and focused request for a development study; a general request to “retest everything” is inefficient.
Build a Comparable-Data RFQ
A request for quotation (RFQ) should include the food application and the evidence the supplier can provide. Define the construction, fill and distribution assumptions, and request reports with the nine comparison fields. Assign acceptance decisions to the appropriate specialists and ask the supplier to identify gaps before quoting a testing program or replacement material.
The worked brief below uses a hypothetical 450 g chilled meal and an 8 × 8 × 3 in target format. Those are example buyer inputs, not a Wonhi performance claim or an approved food-storage specification. Copy the structure into your inquiry and replace the inputs with the requirements established for your product. The range column includes application requirements where no universal numerical range can be recommended.
RFQ checklist: replace the example inputs with your approved application brief.
| Parameter | Recommended range | Why it matters | How to verify |
|---|---|---|---|
| Food and fill mass | Example: 450 g chilled meal; composition to be specified | Food and headspace affect the evaluation | QA supplies the product and filling brief |
| Format and construction | Example: 8 × 8 × 3 in; exact SKU and lid required | Equal size can hide a different liner or closure | Procurement matches drawings, samples and report identity |
| Temperature and route | Actual measured route; no universal temperature range | Laboratory conditions must answer the intended question | QA reviews the time-temperature profile |
| Oxygen and moisture evidence | Report ID; method and edition; units and thickness; temperature; two-side humidity; gas and pressure; replicates and reporting limit | Incomplete reports cannot support a fair comparison | Laboratory completes the 9-Field Barrier Data Match |
| Forming and closure | Actual production sequence, selected closure and tested post-process state | Conversion can change the tested state | Production defines a representative sample trial |
| Food-contact status | Exact construction, food type and intended contact conditions | Oxygen data does not establish material authorization | Supplier returns applicable substance/use evidence; QA accepts or identifies gaps |
| Food shelf-life study | Buyer-defined target duration and quality endpoint; no validated duration assumed | The food and complete pack need their own evaluation | QA defines the study; supplier identifies any matching completed studies and their limits |
| Testing scope and cost | Itemized clarification, material and package tasks | Avoids paying for an irrelevant repeat | Finance approves the staged scope after gaps are identified |
The first decision the purchasing team makes is whether a quoted product is sufficiently identified to evaluate. Acceptance basis is the responsibility of Quality Assurance. Production checks whether the proposed construction can be formed and closed as intended. There’s no generic return-on-investment percent to consider. The Finance team compares the cost to resolve a missing record against the cost of new testing and determines which option is more favorable.
A 2021 IFSQN forum post by a packaging converter states some suppliers give different validity periods for unused plastic packaging. Ask how long the empty stock can be stored, and what the storage conditions are. This is different from the shelf life for the later food that’s filled into it.
The Significance and Use section of ASTM D3985-24 calls for agreement on sampling, test conditions and acceptance criteria. Incorporate this agreement into the quotation.
ASK THE SUPPLIER to return a brief with evidence and untested questions marked up. A helpful response explains the specimen, method and condition, and differentiates a proposed trial from a completed test. This helps define the next step for a sample rather than enter a lengthy debate as to whether a material is “better.”
Key takeaway
Match the report to the exact specimen and conditions, then evaluate the assembled pack and food. BUY evidence that addresses the intent of the application question.
SEND THE BRIEF when discussing Wonhi Meal Box disposable food containers. Include the lid and liner requirements, with the tray format, so the first response can address the full proposed construction.
Discuss your packaging specification
Frequently Asked Questions
What are factors affecting permeability?
Permeability depends on the permeant, material structure, temperature and moisture exposure; thickness and pressure conventions also matter when interpreting a reported value.
Compare the gas permeability and water vapor results separately because they describe different species and may use different methods. Grade, orientation, crystallinity and the presence of coatings can change a film’s behavior. Request the tested construction and conditioning record. A material-family name or a single number without units cannot establish equivalence between two supplier reports.
What types of damage to food packaging would be grounds for rejecting the food?
Packaging that has lost its intended protective integrity should be held from normal use and assessed under the site’s receiving and food-safety procedures.
Visible punctures, an open or damaged closure, unexplained leakage or contamination call for assessment rather than a favorable permeability number. The decision depends on the food and the protection the package is meant to provide. Do not taste food to investigate an uncertain package. Record the damage, isolate the affected items and refer the disposition to the responsible quality or food-safety team. A cosmetic mark on secondary packaging is a different question from damage to the food-contact barrier.
What is the most sustainable food packaging?
Sustainable food packaging must protect the actual food and fit the available collection and end-of-life system; a material name alone cannot establish the best option.
A poor barrier that contributes to food loss can undermine a material-saving change. Conversely, adding layers without a demonstrated need can complicate the design. Compare the materials used, required performance and locally available recovery route. Where producer responsibility rules apply, evaluate those requirements separately. Claims about recyclability or compostability need evidence for the exact construction and destination.
What is vapour permeability?
Vapour permeability describes water-vapor passage through a material with the normalization defined by the measurement.
The US spelling is vapor. Check whether the report gives a transmission rate, permeance or permeability coefficient, then read its units, temperature, humidity difference and thickness assumptions before comparing it.
Can a supplier’s film test report establish the shelf life of my meal?
A film report alone cannot establish the shelf life of a prepared meal because it does not evaluate the complete food, package and process.
A useful report supplies one part of the evidence: how a defined specimen transmits oxygen or water vapor under specified conditions. The meal may also be affected by its initial atmosphere, ingredient interactions, processing, closure quality and distribution route. Moisture can move within the food even when little crosses the outer package. Leakage can create another pathway that a flat-film test never examined. Ask the responsible food specialist to define the product-specific study and acceptance basis, then use material results to support that work. If a supplier offers a shelf-life statement, request the food formulation, package construction, process and study conditions to which it applies. A study on another food or another lid is not automatically transferable. The practical next step is a scoped validation plan, not multiplication of a film value by a desired number of storage days.
How this comparison was prepared
GW prepared this food packaging permeability guide from public test-method scopes, original research and attributed industry sources. The report comparison and RFQ are worked examples of purchasing, not customer trials. Wonhi catalog references identify product constructions only; no private oxygen-transmission, water-vapor or shelf-life results were supplied for this analysis. Lab findings remain with researchers and specimens described.
References & Sources
- ASTM D3985-24: film and sheeting oxygen transmission
- ASTM F1927-20: oxygen transmission at controlled relative humidity
- ASTM F1249-25: water vapor transmission
- ASTM F1307-20: oxygen transmission through dry packages
- Dai et al., 2023: fresh-cut broccoli atmosphere experiment
- Moody et al., 2025: pectin-coated PET films
- Yeh and Turan, 2026: gas-permeability mapping
- Parhi, WSU, 2021: coated-film defect research, public abstract
- FDA: regulatory status of food-contact components
- FDA Import Alert 16-125: reduced-oxygen fish packaging
- IFT: permeability and transmission calculations for multilayer materials
- IFT, Claire Koelsch Sand: controlling moisture
- Packaging World, Sterling Anthony: vapor transmission rates